Description
Glutathione
Introduction
Glutathione is a premium-quality pharmaceutical compound manufactured using advanced production technology and stringent quality control procedures. Produced in controlled manufacturing environments, Glutathione is formulated to deliver high purity, formulation consistency, and dependable manufacturing standards.
Every production batch undergoes comprehensive analytical testing to verify identity, purity, and overall product consistency before release. Carefully packaged using pharmaceutical-grade materials, Glutathione is designed to maintain product integrity throughout storage, transportation, and handling.
Product Highlights
- Premium-quality pharmaceutical compound
- High-purity Glutathione formulation
- Advanced manufacturing technology
- Precision production processes
- Batch-tested for quality and consistency
- Manufactured under controlled production standards
- Comprehensive quality assurance
- Secure pharmaceutical-grade packaging
Product Specifications
| Specification | Details |
|---|---|
| Product Name | Glutathione |
| Category | Pharmaceutical Compound |
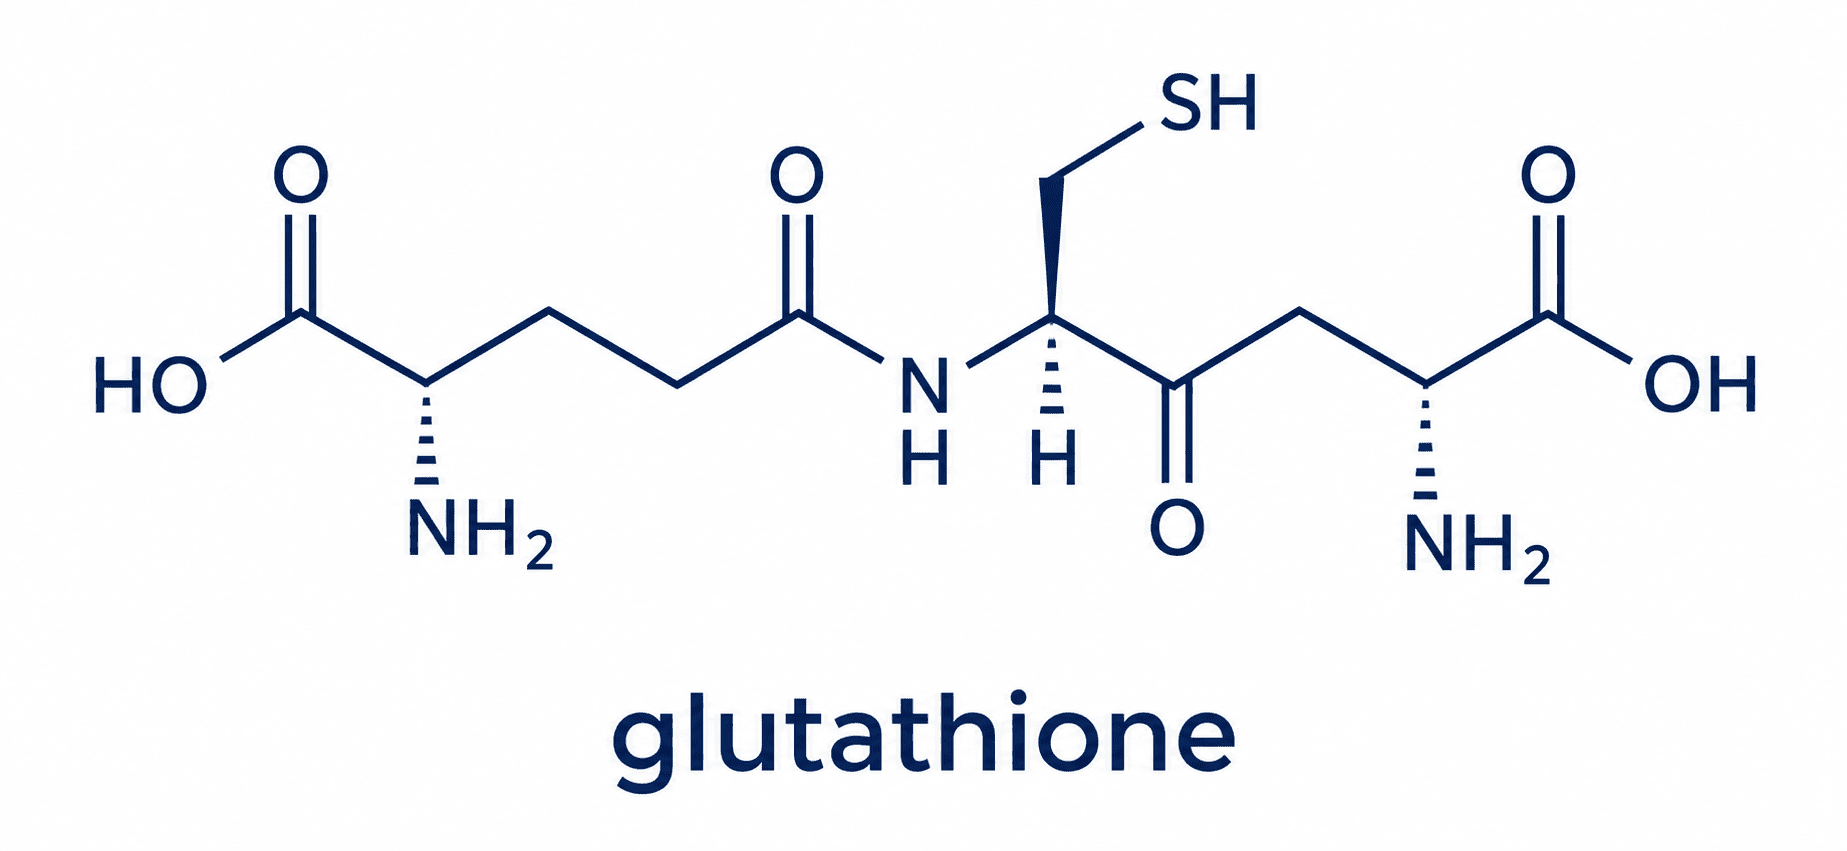
| Chemical Name | Reduced L-Glutathione (GSH) |
| Form | Lyophilized Powder / Injectable Solution* |
| Appearance | White to Off-White Powder or Clear Solution |
| Purity | High Purity (Batch Specific) |
| Packaging | Sterile Glass Vial |
| Storage | Store Refrigerated at 2°C–8°C |
*Product form and concentration may vary depending on the manufacturer.
Manufacturing Excellence
Glutathione is manufactured using precision production techniques and advanced purification technologies. Every stage of the manufacturing process is carefully monitored to ensure formulation consistency, product purity, and reliable production quality.
Manufacturing focuses on:
- Premium-quality raw materials
- Advanced purification methods
- Precision formulation techniques
- Controlled manufacturing environments
- Consistent batch production
- Strict quality management procedures
Quality Assurance
Each manufacturing batch undergoes comprehensive analytical evaluation before release.
Quality testing includes:
- Identity verification
- Purity analysis
- Appearance inspection
- Stability assessment
- Batch consistency evaluation
- Packaging quality inspection
These procedures help maintain dependable manufacturing standards and consistent product quality.
Physical Characteristics
Glutathione is manufactured with careful attention to formulation quality and product presentation.
Typical characteristics include:
- White to off-white lyophilized powder or clear solution
- Stable formulation
- Uniform product appearance
- Sterile vial presentation
- Clearly labeled packaging
Packaging
Each vial is securely packaged to help preserve product quality during storage and transportation.
Packaging features include:
- Sterile sealed glass vial
- Tamper-evident seal
- Product identification label
- Batch number for traceability
- Protective outer packaging
Storage Recommendations
For optimal product preservation:
- Store refrigerated at 2°C–8°C.
- Protect from direct sunlight.
- Do not freeze unless specified by the manufacturer.
- Keep the vial tightly sealed until use.
- Store in the original packaging.
- Do not use if the vial or packaging has been damaged.
Product Advantages
Glutathione is manufactured with an emphasis on precision, quality, and consistency.
Key advantages include:
- High-purity formulation
- Advanced manufacturing technology
- Reliable batch-to-batch consistency
- Comprehensive analytical testing
- Stable product formulation
- Professional pharmaceutical-grade packaging
- Controlled production standards
- Excellent storage stability
Why Choose Premium Quality Glutathione?
Premium-quality Glutathione is produced using carefully selected raw materials, advanced manufacturing technologies, and comprehensive quality assurance procedures. Every stage of production is designed to maintain formulation consistency, product integrity, and dependable manufacturing quality from production through final packaging.
Key quality commitments include:
- Premium raw material selection
- Advanced purification technologies
- Precision manufacturing processes
- Rigorous quality control
- Consistent batch production
- Secure pharmaceutical-grade packaging
- Stable formulation for reliable storage

GHK-CU-50mgTB500-10mgBPC157-10mgKPV-10mg-Blend-500x500.jpg)

Leave a Reply